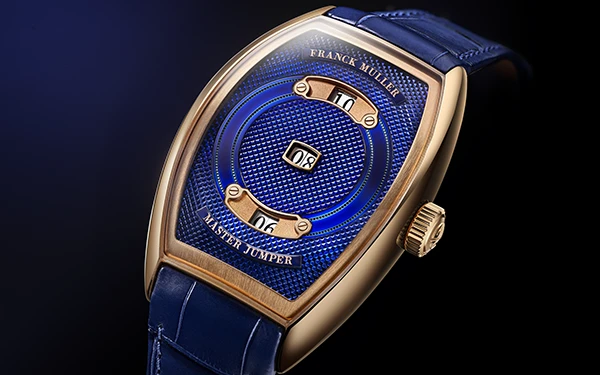

Shortly after its founding, Franck Muller began working on becoming a manufacture, and it wasn't until 2019 that it was completed. The reason it took so long was because they tried to produce as much as possible in-house. There are many manufacturers in Switzerland that boast of having integrated in-house production, but there are not many manufacturers like Franck Muller, which has everything from the design of the interior and exterior, to the manufacture of movement parts, and assembly to final inspection, all concentrated in Watchland.

Interview and text by Masayuki Hirota (Chronos-Japan),
Edited by Yukiya Suzuki (Chronos-Japan)
[Article published in the July 2024 issue of Kronos Japan]
Watchland
Proof of a "Master of Complications"

Pascal Offaud, who worked as a prototyper in the R&D department and was involved in the development of the Aeternitas and other models, said, "Franck Muller has taken an unusual path in the watch industry. Because everything can be done within Watchland, we have a great degree of freedom. This is all thanks to Mr. Golay." As he said, Franck Muller's transformation into a manufacture made great strides under the leadership of master designer Pierre-Michel Golay, who pushed for the in-house production of Watchland from the early 2000s.

Patrick Pellet, also from the R&D department, added, "Before that, Franck Muller's development environment for base movements and unique modules was different. That's why I wanted to make as much as possible in-house. When I joined the company in 2006, we had the Flying T, Revolution 3, Minute Repeater, and even a small tourbillon."

Over time, Franck Muller has grown into a manufacture, and as a result has accumulated a wealth of know-how. Offor revealed an episode related to the Aeternitas Mega.


"When assembling the Aeternitas chronograph, it is impossible to remove play with normal machining precision. Even if parts are made with an EDM, they are unable to make parts with a thickness of less than 0.5 mm. So I cut off just 10 microns by hand."
He casually mentions that even the most skilled craftsman finds it extremely difficult to remove a hundredth of a millimeter by hand, but these "masters" are found throughout the Watchlands.
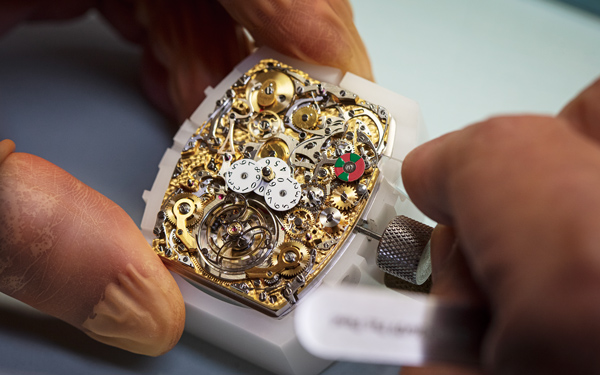
Franck Muller's approach of bringing everything under the watch brand and producing as much as possible in-house has also had a positive impact on the assembly department, as Damien Dest, head of the tourbillon workshop, explained.

"Honestly, there are still just as many problems as before, but we can solve them faster now because design and manufacturing are all in the same place."
The example he gave was the Giga Tourbillon, which has a balance wheel with a diameter of 16.70 mm.
"When we first made the Giga Tourbillon, we realized that the carriage was too large and could not withstand shocks. We immediately contacted the design department, who added a locking mechanism to prevent the pivot from separating from the stone when an impact is applied."

In the workshop where tourbillons are assembled, the barrels were actually being assembled. Normally, mainsprings are purchased already installed, but at Watchland, the delivered mainsprings are assembled into barrels made in-house, and the torque of each is calculated. The person in charge said, "We dare assemble them in-house so that if the torque is incorrect, we can immediately replace them."

In recent years, Franck Muller has begun to use a slip mainspring, which is unusual for a hand-wound movement. While this is less prone to malfunction, controlling the torque is difficult. This is an attempt that only Franck Muller, which inspects every single watch for torque, could undertake. In addition to assembling the barrel, other tasks that other companies would leave to the sub-assembly department were also carried out, such as attaching the latches to the anchor and pallets.

The movement being assembled at the time of this interview was the Grand Curvex Giga Tourbillon, released in 2011. "Because the balance wheel is large, it's not a difficult movement for watchmakers," says d'Est, but that's in comparison to the Aeternitas and similar. The moment of inertia of the Giga Tourbillon's balance wheel is 64.4 mg/cm2 for the original model from 2011, and 69.4 mg/cm2 for the latest version. Even though it's made of lightweight titanium, it still fits into a 20mm diameter carriage. Removing the unbalanced weight and preventing distortion of the axis are no easy tasks.


Of course, the evolution of Watchland is behind the creation of the Giga Tourbillon. Patrick Pellet of the R&D department states that "we are able to use a titanium carriage because we now have the necessary processing equipment." However, since manual refinishing is difficult, it is necessary to improve the processing precision in the first place in order to prevent uneven weight. The processing precision of the balance wheel after cutting is said to be within ±10 microns, which is quite precise.


Additionally, the Complications department also checks the ceramic bearings that support the flying tourbillon. The company has used ball bearings since the Flying T in 2001, but in recent years has switched to ceramics, further improving the precision of the housing that houses the tourbillon.

The company's own FM1700 series is also assembled in the tourbillon workshop. While it may seem simpler than a tourbillon, Dest says, "it's difficult to prevent scratches." Since the watchmakers also set the jewels in the chatons, assemble the regulator (!), and polish them, it's only natural that they can't be left to an ordinary watchmaker. So, what happens if a watch gets scratched?


"We have a decoration department on the floor below the assembly shop, so we can quickly refinish it," Dest says.
Franck Muller has achieved a high level of integration and accumulated know-how under the name of Watchland. Every department is interesting, but what caught my attention the most was the cutting of the carbon case and the storage of the dial.


Currently, most of Franck Muller's cases are manufactured by Jutec, a group company. However, cases for prototypes and small-scale production models are manufactured in-house. One of their newest ventures is the carbon case.
Thanks to skilled workers who have been with the company for many years and new milling machines and lathes, Watchland has greatly improved the precision of its parts. For example, the machining precision of the main plate is said to be within ±2 microns (!), and the precision of the balance shaft, which is finished by grinding, is similar, so Watchland can now be said to be one of the finest watchmaking workshops in Switzerland. In particular, as far as I know, there are hardly any other manufactures that have the know-how to "fine-tune machines using the sounds and vibrations produced when cutting."

Watchland then tackled a new material called carbon fiber. Made of carbon and resin, carbon fiber is a mixed bag in terms of both finish and material. Increasing the amount of resin makes it easier to process, but reduces durability. Conversely, increasing the amount of carbon fiber makes it harder, but more difficult to process. There is also the lingering problem of fibers sticking out.
Franck Muller, which takes pride in its case craftsmanship, chose dense carbon and spent two years mastering the cutting technique. A person in charge said, "Carbon is a material that is easily subjected to stress during processing. For this reason, it is important to process it in a way that does not produce fibers. What is required is experience." I had never heard of fiber-free cutting before, but apparently they changed their tools and lubricants to achieve this. "It takes about two and a half hours to cut one piece, and they can only produce four to five per day," so it is quite a lot of work. Rather than relying on the latest machinery, the craftsmanship is always involved, which is a characteristic of Watchland.

Another highlight is the dial storage facility. The chateau, the heart of Watchland, was originally Franck Muller's workshop. It is now used as an office, with the exception of a semi-basement room attached to the chateau, which is used as a dial storage facility.

Stored here are approximately 7000 different types of dials, totaling approximately one million pieces, manufactured since 1992. In other words, they have a complete collection of the dials that have graced Franck Muller watches. This department is managed by Anna Salis. She was the first employee hired by Franck Muller and Vartan Sirmakes, and she is still involved in production and delivery management. "I'm Franck Muller's first employee," she says with a laugh, but it was surprising to learn that even at a company where employees have been with the brand for a long time, there are still first-time employees.

When I asked her, she brought out a variety of dials. She stocks not only current models, but also Japan-limited editions and vintage chronograph dials. And she even remembers where everything is. Normally, a list would be made and kept strictly managed, but entrusting it to someone else is typical of Franck Muller.

Jutec Co., Ltd.
The precision of the molds that create the ideal case
The biggest reason for Franck Muller's success is undoubtedly the existence of the watchmaker Franck Muller. However, without excellent cases, Franck Muller would not have achieved the success it has today. The company that has supported Franck Muller's designs is the case manufacturer Jutec in La Chaux-de-Fonds. The company's strength is in creating cases by forging rather than cutting. The company has refined a technique that was previously not suitable for three-dimensional shapes, and has now become an indispensable part of Franck Muller.

Franck Muller uses cold-forged (i.e. pressed) cases for almost all of its models. This is an extremely rare approach in an age where cutting is the norm. However, this approach is not surprising when you consider that Franck Muller's co-founder, Vartan Sirmakes, was once a pioneer in forging cases. Sirmakes created the Tonneau Curvex case, which was thought to be absolutely impossible to forge, and he continues to see potential in forging, a method that the Swiss watch industry has largely given up on.
The majority of Franck Muller's cases are manufactured by Jutec, a case manufacturer located in La Chaux-de-Fonds. Founded in 1971, Jutec had been manufacturing cases by forging since shortly after Franck Muller was founded, but was acquired by Franck Muller in 2007. At the time, two companies supplied cases to Franck Muller, but Jutec was chosen because, even though their cases were also forged, they were less likely to develop voids.

Navali Nejib, the company's manufacturing manager, explains the benefits of forging: "Making a case using NC cutting takes a long time. On the other hand, forging saves time, makes the case stronger, and produces a clean surface. On the other hand, it makes the manufacturing process more difficult to control." The step that secures the crystal is a testament to Jutec's current capabilities. While this is usually done by cutting, Jutec creates the stepped recesses using only forging. It is no surprise that Nejib boasts that Jutec is the only company in Switzerland that can do this.

At Jutec, the case prototype is first punched using 54 tons in the case of stainless steel, and then 22 tons of pressure is applied to form the prototype. Jutec is the only company in Switzerland that can press out plates ranging in thickness from 2.5mm to 15mm, so their know-how is unparalleled. The rough shape of the case is then created using 120 tons, the pressure is reduced to 10 tons, then increased again to 20 tons, and finally the case is finished using 50 tons of pressure. Approximately 30 to 40 steps are required to create one case, and it takes about four weeks to complete, making it longer than cutting.

Of course, these processes also include heat treatment. For stainless steel, it is 1080°C for 25 minutes, then lowered to a lower temperature for a total of 40 minutes, and for gold, it is 700°C for 30 minutes. It is amazing that this process is carried out by only three press craftsmen and two people who adjust the machines.
What's interesting is that they try to eliminate the cutting process as much as possible. For that reason, Jutec's workshop sometimes uses a press just to make the case 0.1mm thinner. They are currently trying to create the step on the inside of the case using a press, which is unparalleled in the current watch industry. Incidentally, while the Grand Curvex case has some cutting done on the case, other models generally do not have the outside cut. They must be very confident in their ability to achieve the surface and precision using only forging. In fact, the defective rate for gold cases is zero, and even for stainless steel cases, it is only a few out of 500.

However, with all this technology, Watchland's demands become even stricter. That is the case with the Grand Curvex's titanium case. I had thought that the titanium case was the only one that was machined, but in fact it is forged. "At Jutec, we also forge titanium. The initial press is 60 tons, and the heat treatment takes 10 minutes," says Nejibu. However, in theory, forging a titanium case is extremely difficult. There is probably no other Swiss manufacturer that uses forging.
"It's true that titanium sticks to the mold, so it's difficult to process. That's why we use special oil and raise the temperature before hammering." Jutec, which can even forge titanium cases, is still experimenting with forging new materials. "We were asked to forge a bronze case, but we declined because it was obviously impossible," says Nejibu.

In addition, Jutec has also introduced a three-axis press. This does not apply pressure three-dimensionally, but rather changes the pressure of the press along three axes. This allows three processes to be combined into one. Also, because pressure can be applied in multiple locations, it can be used to make large cases like the Vanguard. It seems that Jutec's approach is to constantly hone its pressing technology.


Furthermore, Jutec's unique know-how is not limited to presses. The manufacturing of the dies required for presses also sets them apart from other companies. Like other manufacturers, they use MIKRON and YASUDA electric melters to press copper masters to create dies. However, the person in charge of dies at Jutec has a career spanning 35 years, which is rare in Switzerland. "We maintain our dies after each use, but they'll be worn out after punching 1000 cases. Incidentally, the copper masters used to make dies have to be discarded if the dimensional tolerance is less than 1/100 of a mm. The dies also have a maximum tolerance of 2/100 of a mm. This results in greater precision than with ordinary cutting."


Jutec boasts an extremely unique process, just like Watchland. What stands out here is the pride of the skilled craftsmen in their work.

Cold forging + heat treatment
Jutec basically forms cases almost entirely through forging. The reason this extremely unique case manufacturing method has survived even in Switzerland is because forging allows for greater precision than cutting. What's more, the company even manufactures the blanks that form the base of the forging in-house. All of this know-how, from how to apply pressure to the temperature and time of heat treatment, has given Franck Muller unique cases.


3-axis press/quality inspection/polishing
Jutec, which has honed its forging techniques, recently installed a completely new press machine. The reason for this is to forge large cases. Despite being pressed, the cases have an incredible precision of within 0.03 mm, which is the result of the company's commitment to achieving greater precision through forging than through cutting. As a result, Jutec's cases are now of higher quality.


Mold
The key to forging is the mold. While mold know-how has become rare in the Swiss watch industry, it remains strong at Jutec. The molds are manufactured with an accuracy of 1/100 mm, and maintenance is carried out after each press, supporting the precise finish of the cases. Moreover, the company keeps a complete stock of molds for past models, with an eye toward future maintenance.


Phil Darnold Lindale, Inc.
The secrets behind dial-making that make Franck Muller
Phil Darnold Lindale has been manufacturing dials for Franck Muller since the brand's early days. This company, which produces dials for luxury watches, has used its technical capabilities to significantly change Franck Muller's dials since becoming a subsidiary of Franck Muller. The basic process remains the same for many dial manufacturers. However, the differences that can be seen here and there give Franck Muller dials a unique personality.

Franck Muller's iconic dials, featuring a highly curved tonneau curved case and bold Byzantine numerals, are the defining features of the brand. These dials are manufactured by Phil Darnold Lindale, a subsidiary of Franck Muller. Founded in 1974, the company initially supplied dials to a few jewelry brands, but became part of Franck Muller in 99 and now produces dials exclusively for Franck Muller and Backes & Strauss. With 100 employees, the factory is quite large for a dedicated dial factory.
The company's director is Alain Vionnet, who was previously an automotive engineer before being invited to join the company by the Boyat family, who acquired the company. He built a career as a mechanic and is now the company's director.

"In the late 90s, Franck Muller was looking for a new dial manufacturer. By chance, Boya's nephew worked for Franck Muller, and Lindale began making the dials."
Since then, Lindale has produced at least 3 different dials for Franck Muller. For the 2024 new product alone, they created 650 different dials. The company's strength is, needless to say, its thick enamel-painted dials. However, over the past 10 years, they have also begun to use PVD finishes. The reason for this accelerated adoption of new technologies is thanks to Tristan Cattan, head of the technical department. With a degree in microtechnology and manufacturing processes, he joined Lindale, a local company, and is driving its innovation. The blend of craftsmanship and cutting-edge technology seen at Lindale is exactly the same as that seen at Watchland and Joutec.

The first thing that surprised me was the process of stamping the guilloched dial. To create the guilloched pattern on the dial, an electric press from the 1950s is used. Hydraulic presses are unable to create fine patterns, so the guilloched pattern on the dial of the Grand Curvex can only be clearly produced with an electric press. After that, the round blank is cut out to fit the case, and fixing feet are attached. Here too, old machines from the 50s are used.
Once the dial has the base attached, it is then significantly bent in the next process before being sent for plating and painting. At Franck Muller, coloring is done by plating, PVD, or painting, and then a protective clear coat is applied on top, about 20 to 40 microns thick. The painting process is partially automated to save labor, but it is still meticulous, with the dials kept in a constant temperature oven heated to 140°C for at least eight hours to completely remove the paint solvents. A person in charge says, "You can't make a good dial unless you respect time."

The process of making the applied Byzantine numerals in this workshop is perhaps the most Franck Muller-esque. Amazingly, all the indexes are not made from plates with attached feet, but are machined from brass blanks, including the feet (!). The indexes are carved out using a machining center. The reason for choosing this time-consuming process is to ensure precise installation. The machined indexes are bent either by automatic machine or by hand, and then polished to a mirror finish. This process was almost unheard of 10 years ago, but has apparently become more common in recent years in pursuit of a three-dimensional effect.
Additionally, Lindale has begun adding color to the applied indexes. While plating the indexes would be a simple solution, they chose to paint them by hand to create a more voluminous look. Even for a skilled craftsman, this process takes at least 15 minutes, making it a considerable effort.

The distinctive shine of Franck Muller dials comes from the time spent polishing them. For example, in the case of dials with a soleil pattern, the base is polished to a mirror finish before bending. The reason for this is that it is difficult to add a finish after the pattern has been applied. Normally, polishing is not done after priming, but by deliberately polishing the applied indexes after priming, and then masking the base before applying other plating, a two-tone relief dial is created. As a result, the applied indexes and the dial blend in beautifully.

What was surprising was the PVD treatment process that was set up in one corner of the company. "Normally, when PVD is used, the color is often blue or brown. But 99% of the dials here are noir (black)," he said. Lindale, which has lacquer technology, has been working on PVD-treated dials since 2014 in search of a more matte finish. Who would have imagined that some of Franck Muller's black dials would be made with PVD, a finish that is finally becoming widespread in the watch industry?
The unique dials are the result of skilled craftsmen and cutting-edge machine tools. The slogan "Master of Complications" is in fact the culmination of the work of these masters.
1. Stamping

Like Jutec, Lindale also used presses. The photo above shows an electric press used to punch out dial blanks. It was made by Ostweiler in the 1950s. This press is used to punch out round blanks and also to create patterns on the dials. Because the force is applied gradually, the load on the molds is small.

2. Footing

The dial is first cut with a 6-ton press to fit the case. Then, the feet are attached to the jig or movement. Automatic feet-attaching machines were introduced for mass production, but even today, the feet are attached by hand for small-lot production models. The feet are soldered in place with a PUETSHI tool made in the 1950s, and then caulked to secure them in place.
3. Bending

Once the feet are fixed and holes are drilled, the dial is bent to fit the case. The dial is placed on a jig, a thin rubber plate is placed over it, and the bend is slowly applied with a gentle pressure of about 2 tons. There are three presses used for bending, and the machine used is changed depending on the thickness of the dial.

4. Plating

Lindale also does plating in-house. The main colors they can produce are gold, silver, and rhodium. Black is also possible, but it is not completely black and does not work well with the lacquer applied to the surface. Including the process of immersing the dial in the dissolving solution shown in the photo, it takes 150 to 200 steps to complete one dial. However, half of the dials are discarded, and another 20 to 30 percent are rejected at Watchland, so only about 20 to 30 percent of the dials are usable.
5. Painting

Colors other than gold, silver, and rhodium are generally applied by painting. Lindale currently uses a combination of automatic painting by machine and hand painting. After painting, the dial is left to rest in a constant temperature oven at 140°C for eight hours to completely evaporate the solvent. On the other hand, plated dials are sprayed with a layer of clear enamel about 20 to 40 microns thick to protect the surface. The paint is made by Bellac.
6. Printing

The printing is then transferred onto the painted or plated dial. Semi-automatic machines have been introduced, but the process is still largely done by hand. Generally, the ink is transferred twice, but this is also left to the discretion of the worker. The printing is then baked onto the dial at a low temperature of 80°C. Normal printing takes about 30 minutes, while large Byzantine numerals take about 2-3 hours. According to a person in charge, "printing on a dial with uneven surfaces is extremely difficult."
7. Typesetting
In recent years, Franck Muller has favored applied Byzantine numerals. Normal applied indexes have two legs attached. In contrast, Lindale carves the indexes, including the legs, out of a block of brass (❷). This difficult process was deliberately chosen to ensure the legs are positioned precisely. The indexes are 0.3mm thick and the legs are 0.7mm long, but the leg thickness varies from 0.2mm to 0.5mm depending on the size of the index.
Steps 1 to 4 are the processes for processing and polishing the indexes. The cut-out indexes are fixed to the disc with glue and then slowly buffed from above to create a mirror finish. The glue is then peeled off, the indexes are removed, and then they are fixed in a special jig and plated to complete the process (3). The person in charge explains that because there are so many steps involved, the yield is very low.
Steps 5 to 8 are the process of attaching the indexes. Twelve craftsmen insert the index feet into two holes in the dial, adjust the bend, and fit them tightly to the dial (5). The feet that protrude from the back of the index are then filed down to fix them to the dial (8). Step 7 is the back of the dial with typeset. Only skilled craftsmen can complete the process in just five minutes.


8. Index Painting

To enhance the applied Byzantine numeral indices, Lindale has begun applying a layer of paint to the indices on some models, which requires applying a syringe full of paint to the indices, a process that takes about 15 minutes.
"The colors mustn't flow, and we have to create a thick layer. Getting the viscosity right is difficult," says Jerome Santos, the person in charge. Once the colors are layered, they are fixed in place by heating to 80°C, just like printing. In the photo above, the left index has a border so the paint won't flow, but the right index has no border, so the paint stays on the index due to surface tension.
9. Dial Smoothing

The soleil-finished dial is one of Franck Muller's specialties. For these models, the base is polished to a mirror finish before the dial is processed. This is because if a mirror finish is applied after the pattern has been created by pressing, the unevenness of the pattern will become shallow. The flat dial before molding is fixed to a rotating jig, as shown in the photo above, and polished to ensure the buff hits the surface evenly. This is a simple but very important preparation step.
10. Dial Polishing

The process of polishing the dial of the Grand Curvex Piano. The dial is fixed to a jig (bottom right) and polished three times to give the enamel-painted dial a mirror finish. To make the dial flat, 150 microns of paint, which has been applied over 20 times, is removed, making the process more like grinding than polishing.
To avoid distortion caused by manual work, an automatic machine made by RECOMATIC is used for the final polishing process (top left). This involves placing the dial against three discs at different angles to polish it, and Lindale introduced this process 10 years ago. The polishing itself takes just two minutes, but to prevent the enamel coating from melting due to the heat generated during polishing, a generous amount of oil is applied, similar to cutting (top right). The bottom left shows the dial before polishing. Note the thickness of the enamel coating.
11. PVD

Recently, matte black dials have become prominent in Franck Muller watches. Lindale began developing PVD in 2014 and is now producing black dials. The PVD machine is a FLEXCOAT HYBRID manufactured by Hauser in the Netherlands.
Miguel D'Arrocha, who is in charge of the process, explains, "This machine can accidentally produce different colors, but basically it can only produce black. It takes about eight hours to fix the color to the dial." He adds, "(PVD) is stronger than plating and has a good fixation rate, but it takes 30 minutes to adjust the machine." He also says that half of the dials produced are defective. "After six months, the trash can is full of defective products," he says.

http://www.webchronos.net/features/96949/
http://www.webchronos.net/features/114033/
http://www.webchronos.net/features/105502/