
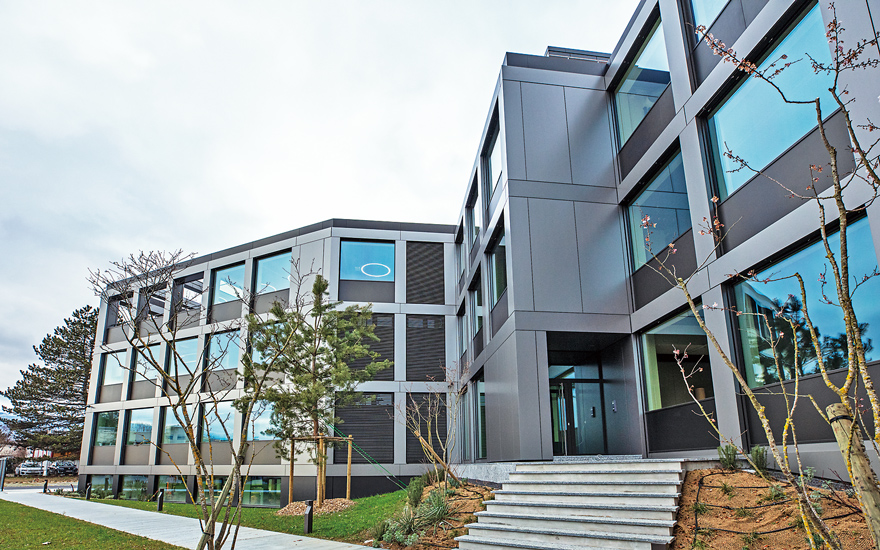
Boitiers Genève, which manufactures FP Journe cases, and Cadraniers Genève, which manufactures dials, moved to a new building at the end of 2022. The building has a total floor area of 2500 m2. Cases are manufactured on the first and second floors, and dials on the third and fourth floors. FP Journe watches already had excellent exteriors, but the expansion following the move is sure to further improve their quality.
Interview and text by Masayuki Hirota (Chronos-Japan)
Edited by Yukiya Suzuki (Chronos-Japan)
[Article published in the July 2023 issue of Kronos Japan]
A completely new manufacturing process brings unprecedented shape and quality
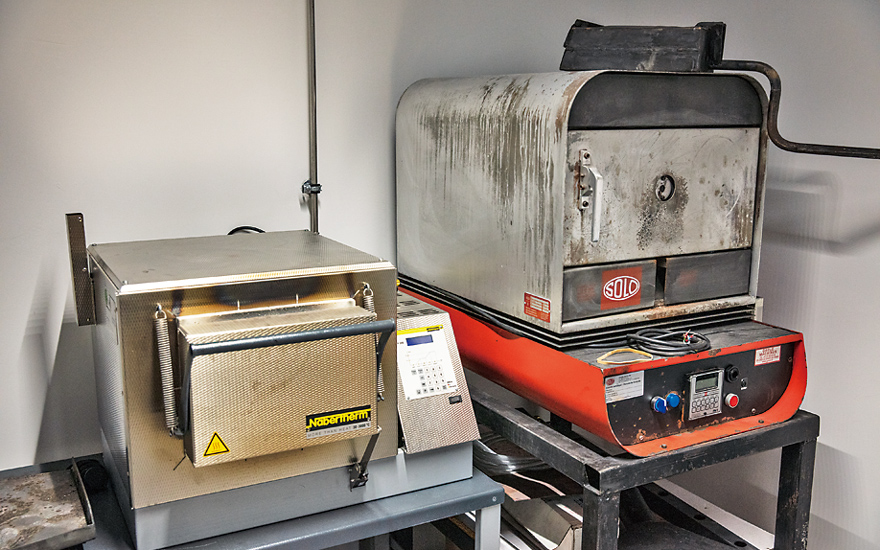
After acquiring a dial manufacturer in 2005, FP Journe then acquired case manufacturer Ellinor. In 11, FP Journe relocated the company, along with its facilities, to Geneva and changed its name to Boitiers Genève. The difference from 10 years ago is the manufacturing method. When the company first moved, precious metals were forged into cases, but now cutting is the norm. The reason for the revamped case manufacturing method is, of course, quality.
Just like high-end Swiss manufacturers, the forged blanks are machined and finished into cases, but each step is meticulous, reflecting the limited annual production of less than 1000 pieces.
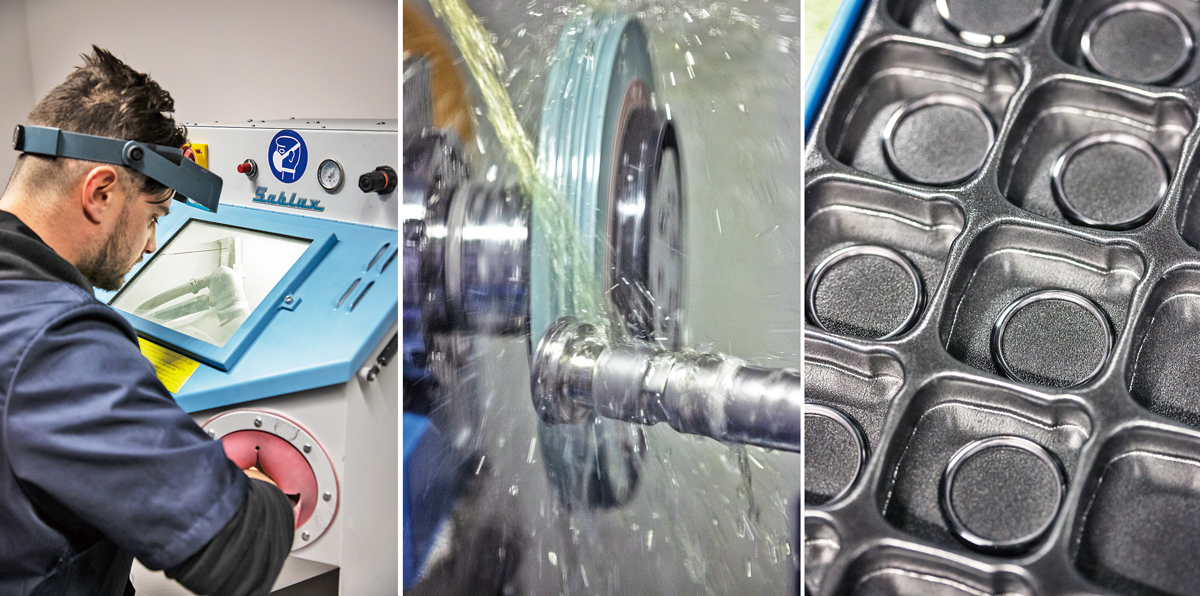
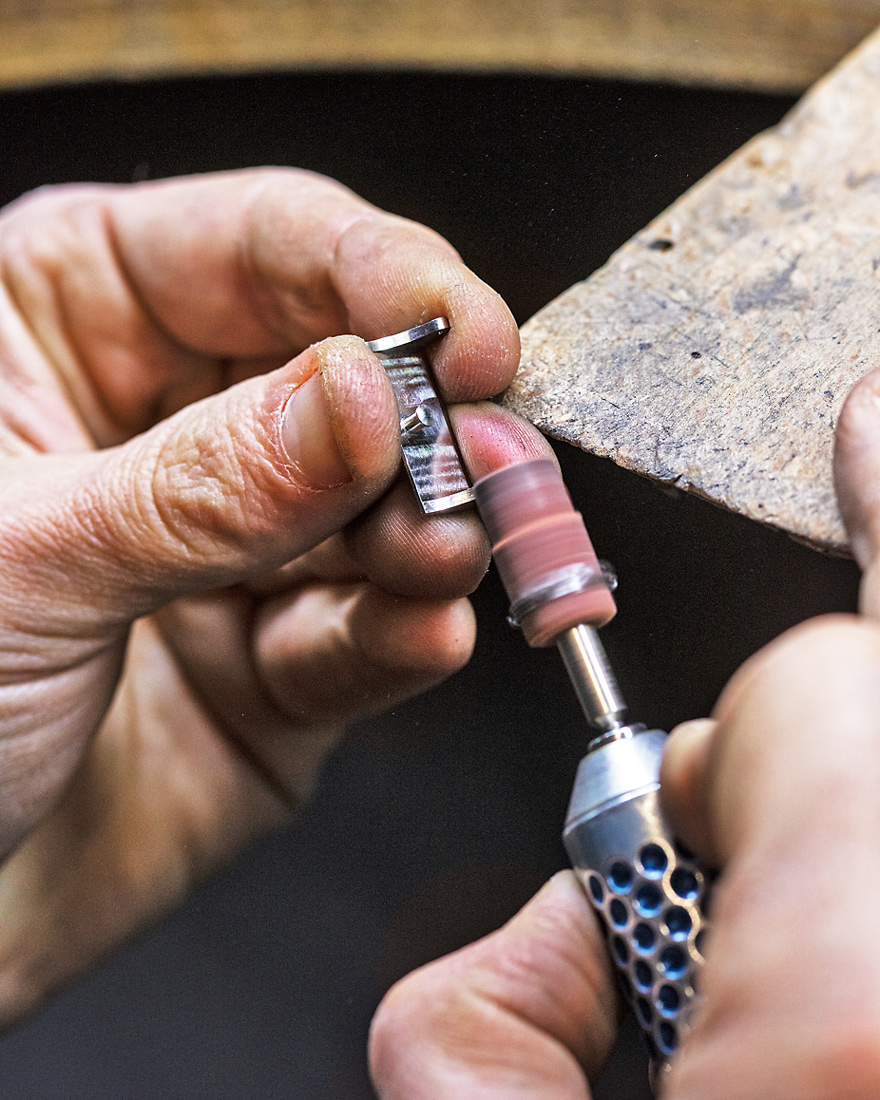
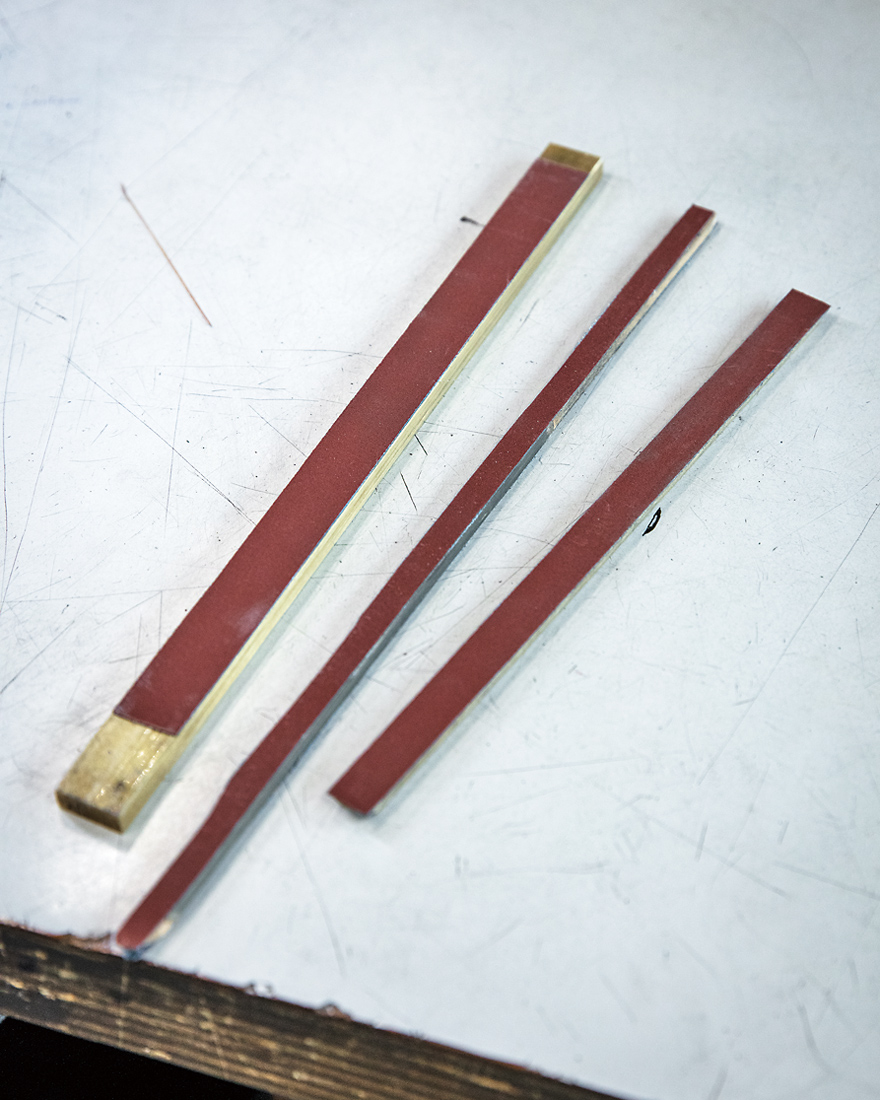
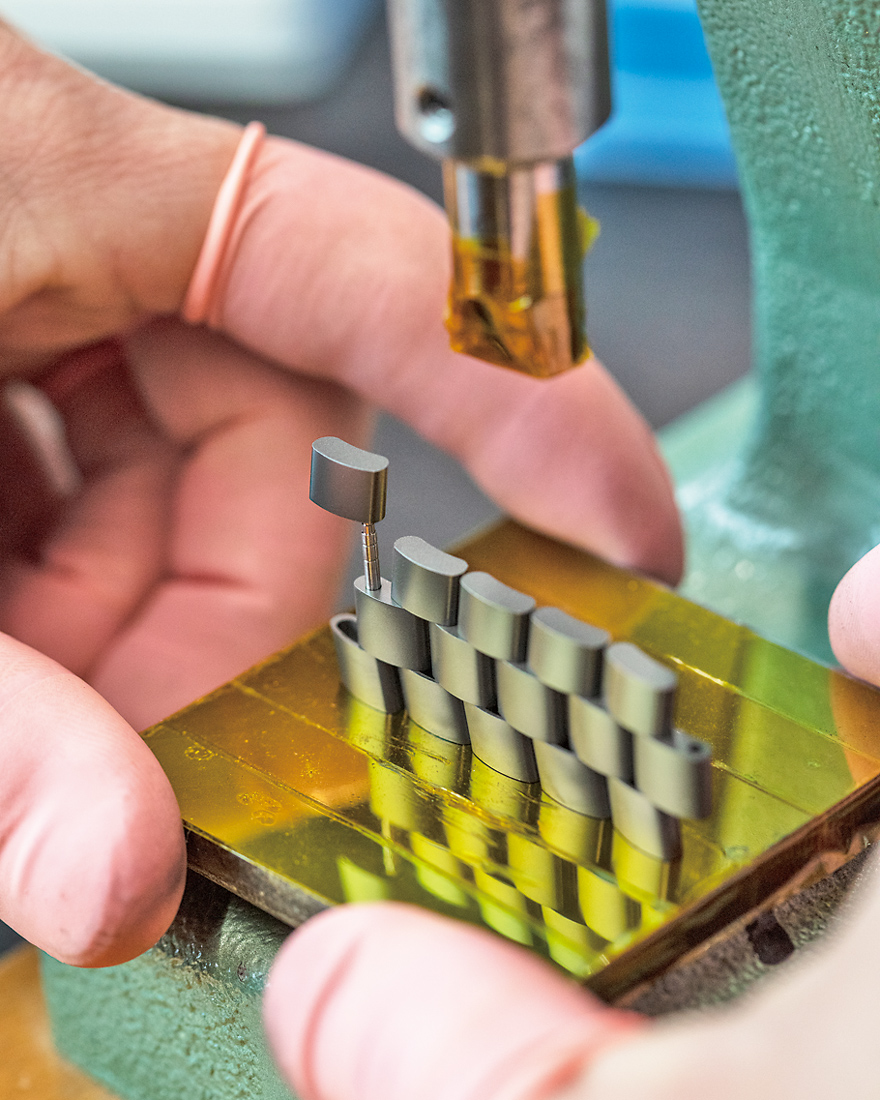
What caught my eye on the first floor was the deburring process. First, the base is smoothed using sand or corundum, and then glass is sprayed onto it to prepare the base. In another department, the tantalum bezels used in the Chronometer Bleu are being prepared. Craftsmen use several types of whetstones to meticulously smooth the surface of the case. Incidentally, polishing tantalum, which is a sticky material, requires re-sharpening the tools after each operation. However, since 2017, progress has been made in mechanizing the process, which has apparently reduced the amount of work required.
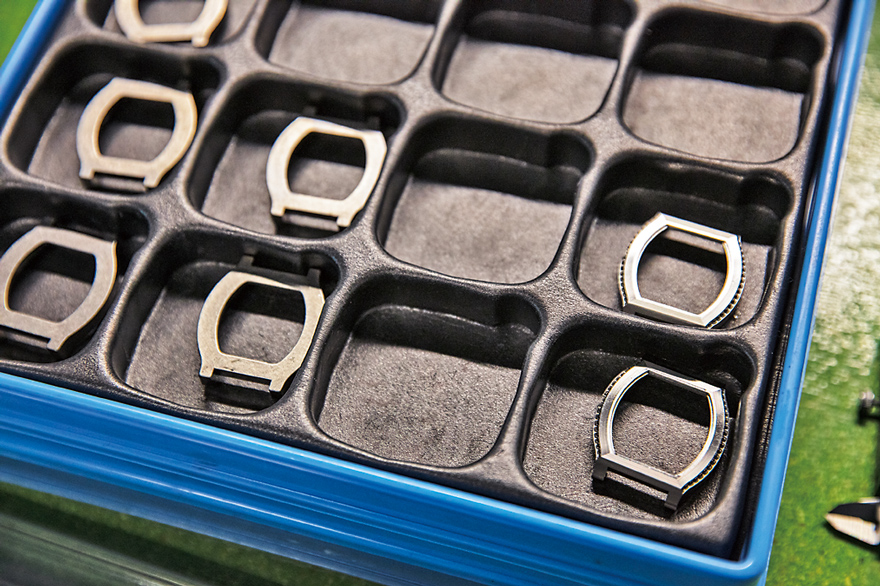
As with the functional parts, machining centers from Fanuc and Wilmin were widely used for the case manufacturing. The slow cutting speed and precise measurements using Renishaw measuring units are also used. However, the processing is said to take a considerable amount of time. It takes 7 to 8 hours to complete the case of the Tourbillon Souverain, plus an hour for setting, so it is not at all suitable for mass production.
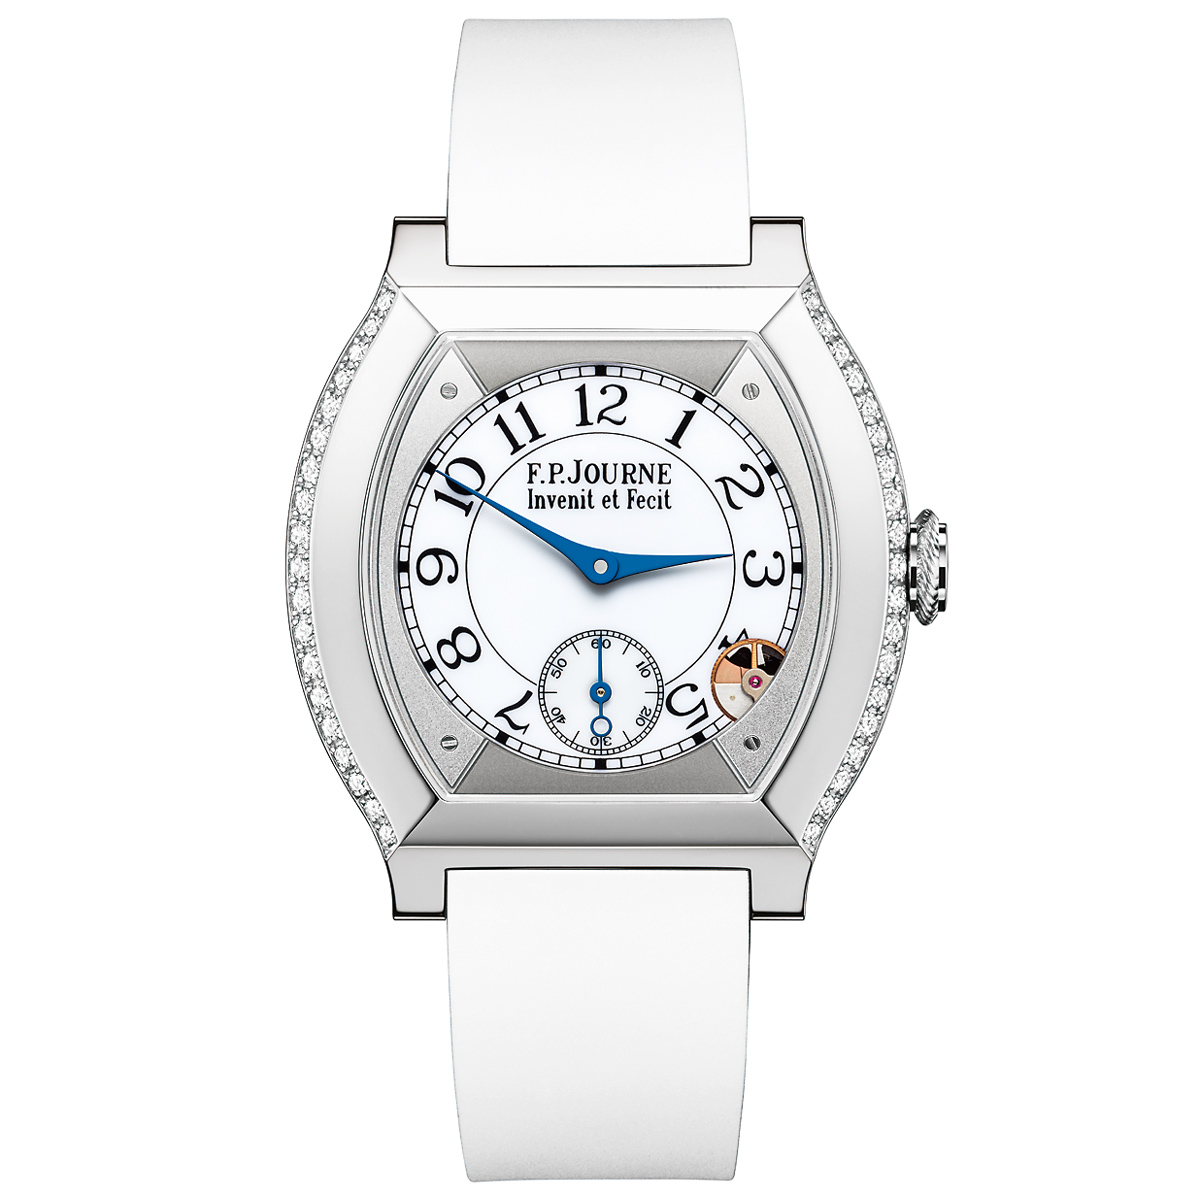
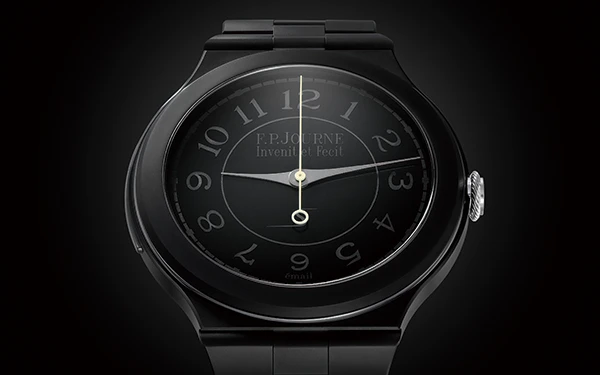
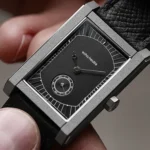
This model features a titanium case set with 38 diamonds. The in-house developed mechanical quartz movement goes into standby mode after approximately 30 minutes of inactivity to extend battery life. The in-house dial is made of sapphire crystal lined with luminous paint. Mechanical quartz (Cal. 1210). 18 jewels. Ti case (40mm x 35mm, 7.35mm thick). Water resistant to 3 ATM. Price: 2,816,000 yen (tax included).
However, this effort clearly improves the finish. As the person in charge explains, "It's important to use the best tools and process faithfully to the design," the high precision of the case has transformed FP Journe watches from high-quality watches for connoisseurs into unique luxury watches.
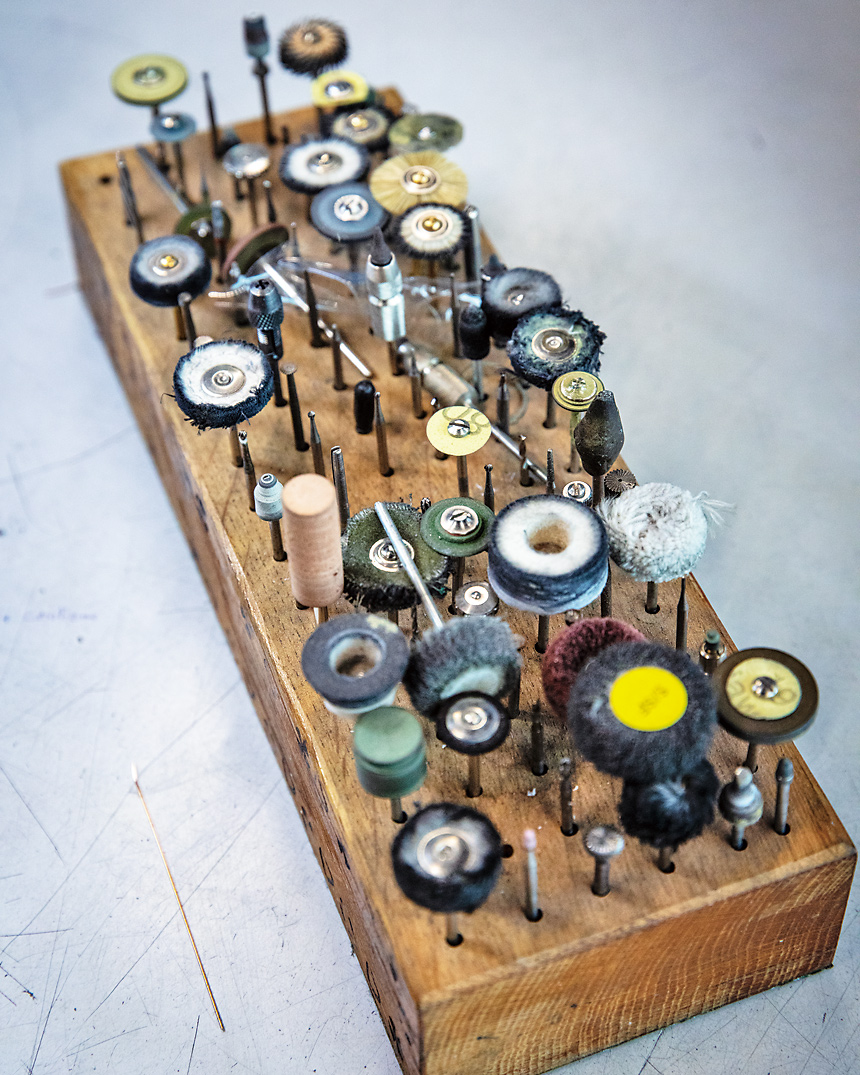
The tools used to make the cases are various, including rubber, paper, sponge, etc. However, the choice of tools and new technologies, not just for preparation and finishing, is left to the discretion of the individual on-site, and only after thorough testing is they adopted.
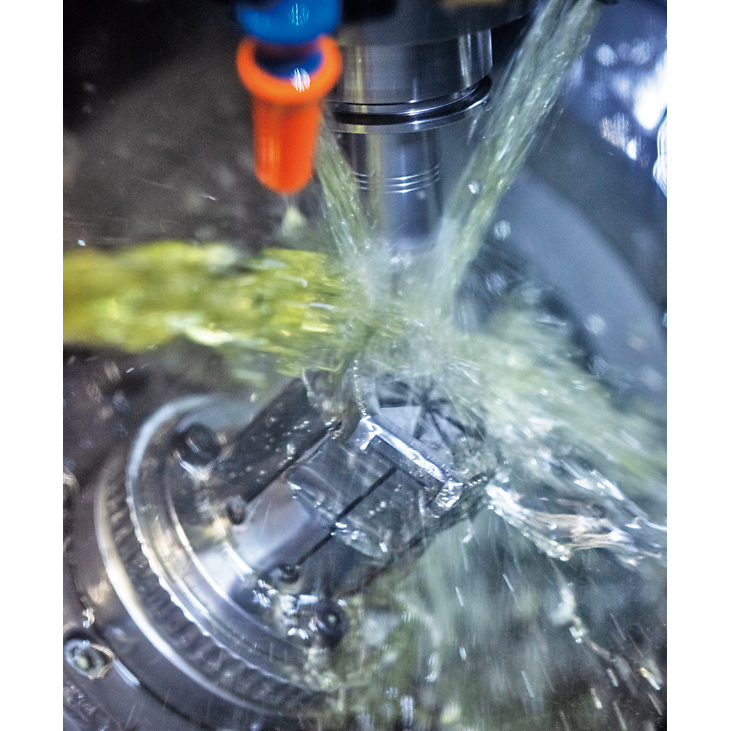
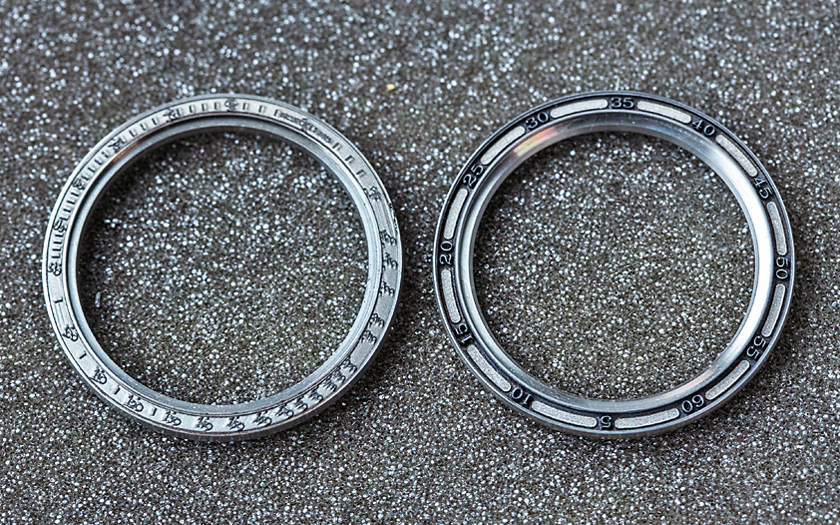
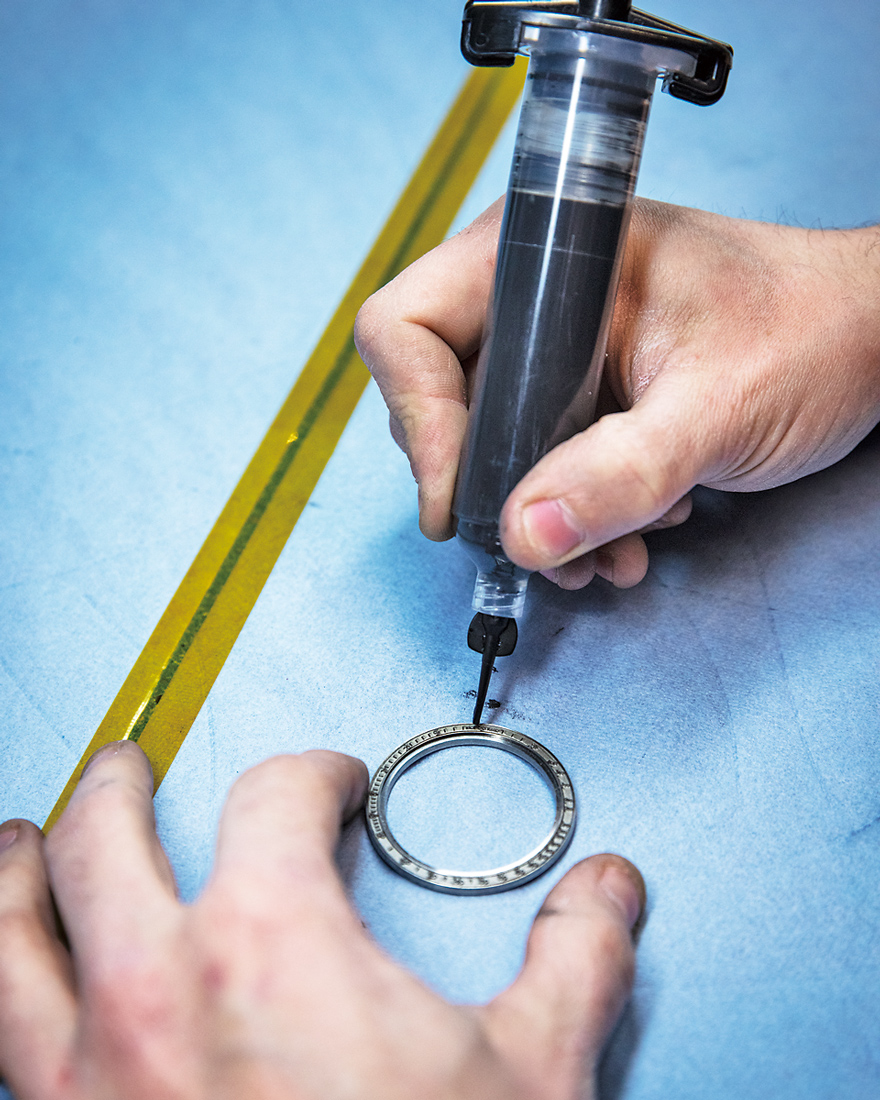
One such attempt that proved successful was the introduction of lasers in 2012. For example, a titanium bezel is engraved using a laser machine that can engrave to a depth of 2.5 mm, taking an hour and a half. In recent years, the engraving has also been filled with liquid ceramic. The manufacturing process is quite elaborate.
The laser-engraved parts are then roughened by sandblasting, then filled with liquid ceramic, heated and pressurized to remove any air bubbles, and then immersed in the liquid for an hour. The surface is then milled away, completing the ceramic-filled titanium bezel. It's an astonishing amount of work, but that's precisely why Journe's genius ideas are finally realized.
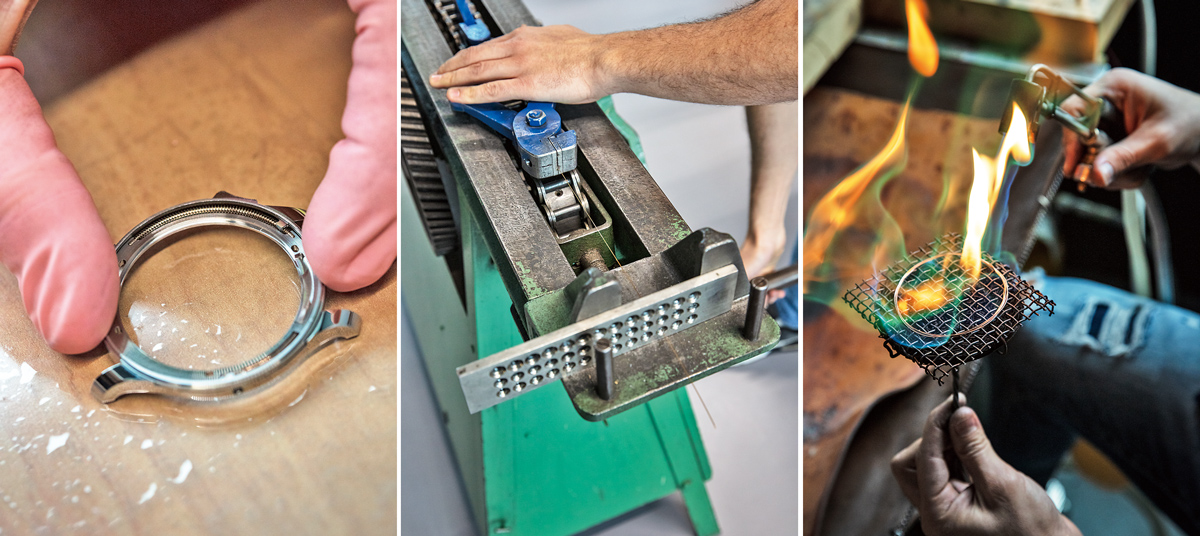
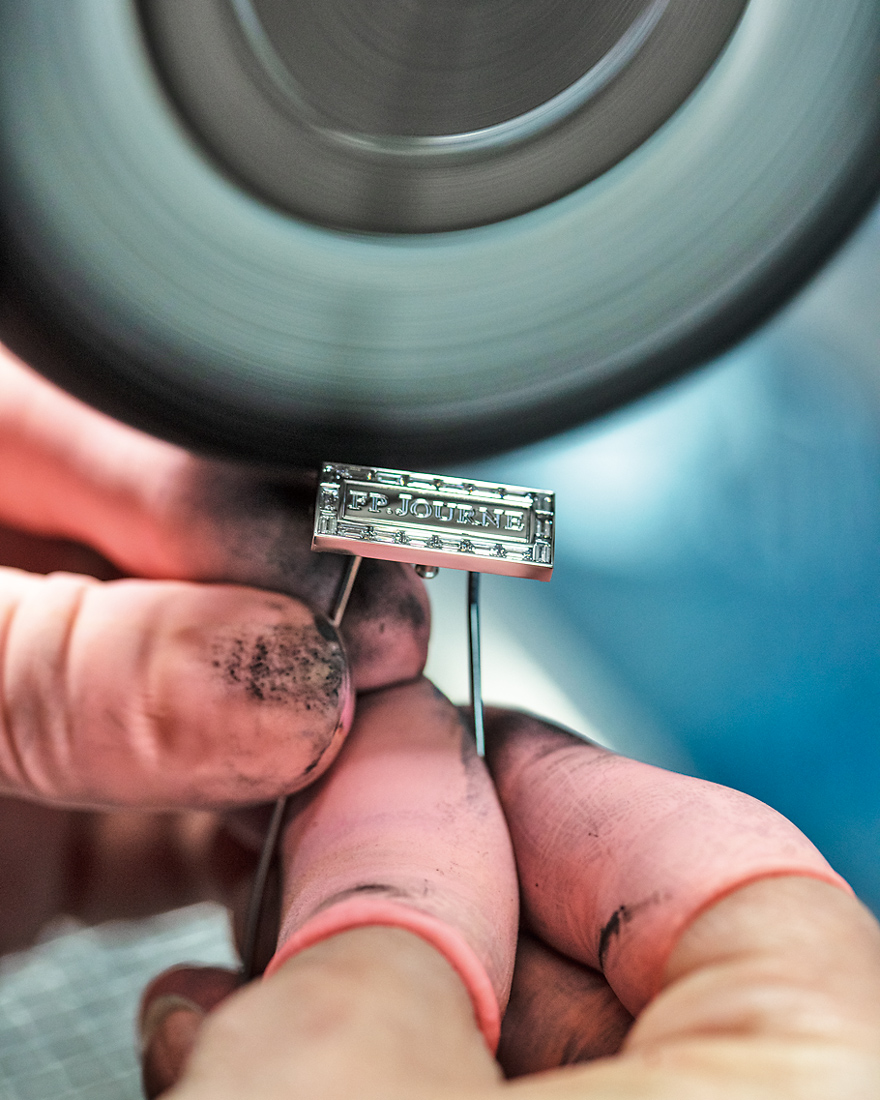
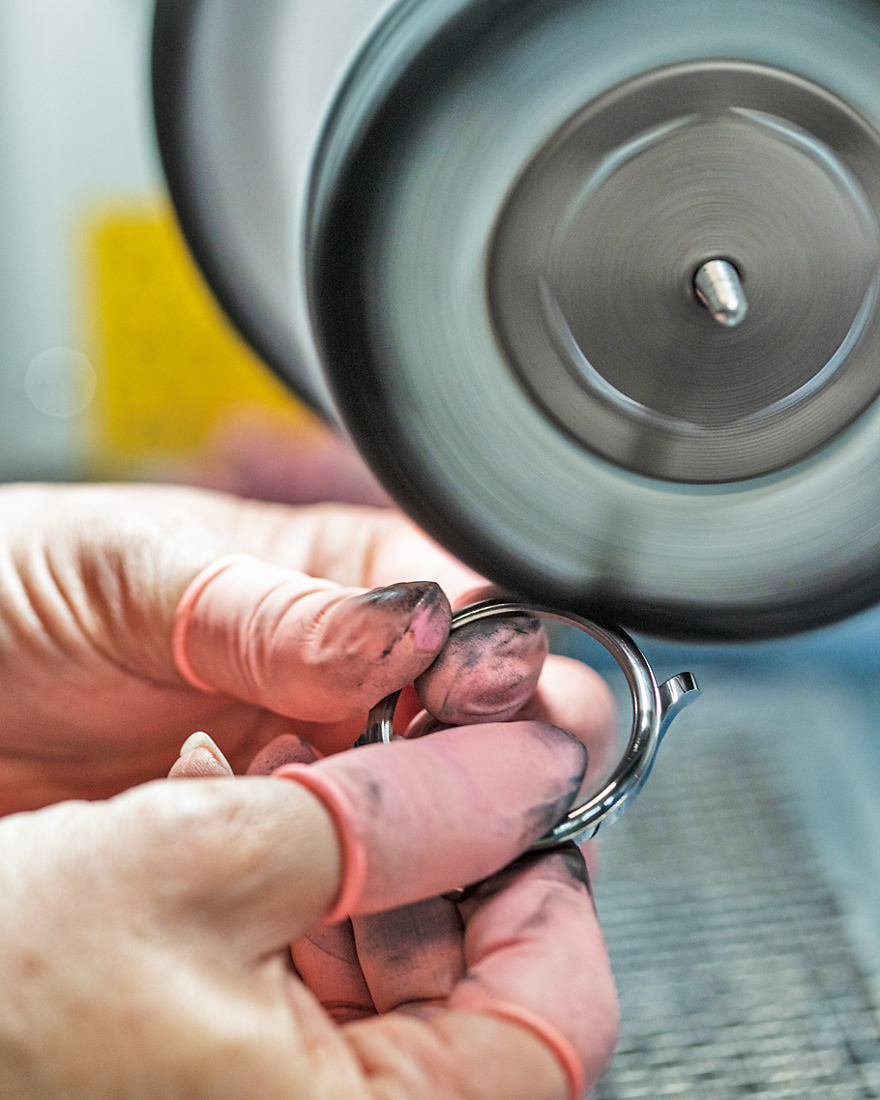
Once cutting and pre-processing are complete, the final polishing process begins. At the time of our interview, the tantalum case was in the final stage of processing. However, unlike gold and platinum, the pre-processing process seems to polish the case almost completely. Like other companies, the case is placed on a rotating buff, but the buffing speed is varied - 1600 rpm for gold, 1800 rpm for platinum, and 2400 rpm for tantalum. The trick with tantalum is to apply slight pressure.
The person in charge of polishing said, "As a result of improvements in the metals used for the cases and the precision of the cutting, the quality of the final finish has also improved compared to before." However, the current FP Journe does not stop there. "The quality has improved overall, but we are currently considering improvement processes to further improve it," he said. Not only has the manufacturing process been completely revamped to ensure quality, but further improvements are continuing. This is the current FP Journe.
http://www.webchronos.net/features/91928/
http://www.webchronos.net/features/76482/
http://www.webchronos.net/features/89473/